Corrugated cardboard is the most engineered commodity in packaging: two liners sandwiching a fluted medium, where the flute geometry and wall count determine how much the box stacks, cushions, and costs. Buyers who understand the grade system stop over-paying for double wall they don’t need — and stop having single-wall boxes arrive crushed. This guide covers grades, box styles, sizing, and the e-commerce economics of corrugated.
If your buyer is asking for FSC-certified board, read our EUDR-ready buyer’s guide to custom packaging boxes — it separates what the regulation actually requires from what a certificate can and cannot promise.
Walls: single wall (two liners, one flute) covers most products up to roughly 15–20kg; double wall adds a second flute layer for heavy or stack-loaded freight; triple wall is pallet-and-machinery territory. More wall is not automatically better — it adds cost, weight, and cube. For the difference between corrugated and folding carton (paperboard) applications, see the box types comparison.
ECT and BCT: Reading the Grade Stamps
The stamp on a box flap carries its engineering spec. ECT (Edge Crush Test) measures stacking resistance of the board itself — 32 ECT is the common single-wall grade, 44–48 ECT typical for double wall. BCT (Box Compression Test) measures the finished box’s top-load capacity, which is what actually matters if your boxes will be stacked in a warehouse or container. Specify by BCT when you know the stack height; specify by ECT when comparing board quality. A serious packaging manufacturer will run compression tests on your actual box design rather than quoting generic grades.
Box Styles and Sizing
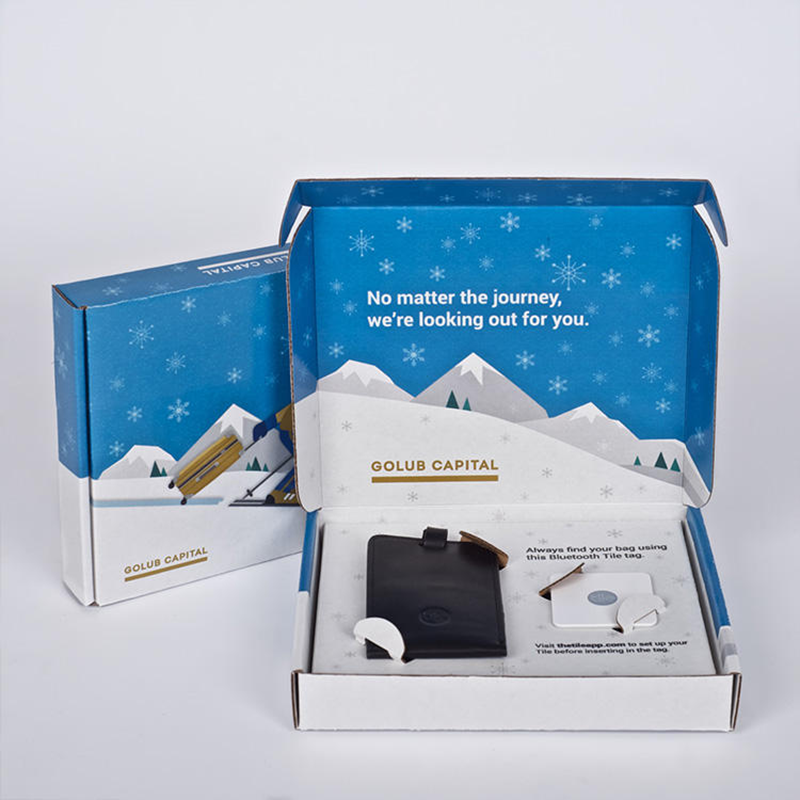
The RSC (Regular Slotted Container) is the economical default — all flaps the same length, minimal waste. Mailer boxes (one-piece tuck-top with friction locks) are the e-commerce unboxing standard. Die-cut boxes add custom features — handles, dispenser openings, internal partitions — at tooling cost. Sizing rules: order by internal dimensions with 2–3mm clearance around the product plus any void fill or insert; and size the box to the product, not the product to a stock box, because shipping carriers now charge by dimensional weight.
The E-commerce Math: Dimensional Weight
Carriers bill the greater of actual weight and dimensional weight (length × width × height ÷ a divisor, typically 139 for domestic US parcel). Practical example: a 30×30×30cm box has a dimensional weight near 2kg — if your product weighs 300g and ships in that box, you are paying air freight rates for empty space. Right-sizing a box by even 2–3cm per side routinely cuts per-shipment cost 10–20%, which across thousands of parcels dwarfs any unit-price negotiation on the boxes themselves. Custom-sized corrugated at volume costs little more than stock sizes — the economics of e-commerce shipping packaging reward precision.
Printing on Corrugated
Direct flexo handles logos and 1–3 color branding economically — the standard for shipping boxes. For photographic retail-facing graphics, litho-lamination (offset-printed sheet mounted to the board) delivers magazine-quality faces on corrugated strength. High-definition flexo covers the middle ground. For industry-specific structures — produce, pizza, electronics — see corrugated boxes by industry.
Frequently Asked Questions
Single wall or double wall — how do I choose?
Single wall (32 ECT) for products under ~15kg without heavy stacking; double wall when boxes stack in warehousing, ride ocean freight, or exceed ~20kg. If your damage claims come from crushing in transit stacks rather than impact, that is a double-wall signal. When unsure, ask for BCT numbers against your actual stack plan.
What does 32 ECT mean on a box?
Edge Crush Test of 32 pounds per inch: the board resists 32 lb of compression per inch of edge before failing. It is the standard single-wall workhorse grade. 200# test (burst strength) is the older alternative rating for a similar grade — ECT is the more useful number for stacking applications.
Are corrugated boxes recyclable?
Yes — corrugated is among the most recycled materials in existence, and old corrugated containers (OCC) feed most recycled paperboard. Keep the spec clean: paper tapes instead of plastic, water-based inks, and minimal plastic laminates preserve both recyclability and the lower eco-modulated fees now charged under US state EPR programs — context in sustainable box solutions.
ISTA Testing: When You Need a Certified Transit Test
Most corrugated specifications are derived from experience and a rule of thumb. That works until a product starts arriving damaged, a marketplace demands evidence, or a carrier disputes a claim. Then you need a test, and the recognised framework is ISTA.
What the tests are. The International Safe Transit Association publishes a family of procedures. ISTA 1-series tests are non-simulation integrity screens — drop, vibration, shock — and are the cheapest way to compare two packaging designs. ISTA 2-series combines partial simulation with the same basic tests. ISTA 3-series is full simulation against a measured distribution environment and is what most large retailers and carriers ask for.
When it is worth the money. A full 3-series test costs real money and takes days. It earns that when the product is high value, fragile, heavy or already generating damage claims — and when a customer contract requires it. For a low-value product in a standard shipper, a 1-series drop and vibration screen on two candidate boxes usually answers the question for a fraction of the cost.
What a test actually tells you. Not “this box is strong enough” but “this combination of box, cushioning, closure and pack-out survived this specific sequence”. A pass applies to the exact configuration tested. Change the void fill, the tape or the orientation, and the result no longer holds — which is the most common way a passed test gets invalidated in production.
Test the pack-out, not the carton. Damage almost always originates at the interface between product and box, not in the board. Adequate void fill so nothing moves, a closure that survives a drop, and no product sitting directly against a seam will do more for your damage rate than moving up a grade of board. For industry-specific corrugated choices see custom corrugated boxes by industry.
Right-Sizing: Cutting Dimensional Weight Without Losing Protection
Carriers bill on the greater of actual and dimensional weight, which means a large light box is charged as if it were heavy. The lever is volume, not board grade.
Do the arithmetic. Dimensional weight is length × width × height divided by a carrier-specific divisor. On a typical international divisor, a box 10% larger in each dimension is about 33% larger in volume — and the freight bill follows. Two centimetres of unnecessary height across a product line is a real annual cost.
Where the wasted space is. In practice it comes from three places: a box size chosen from a supplier’s standard list rather than from the product, void fill used to compensate for a box that is too big, and a height driven by the tallest variant in a range rather than by an insert that adapts.
The protection trade-off. Shrinking a box reduces the cushioning distance between product and wall. The limit is the product’s fragility: below about 25–50 mm of protective clearance, drop performance falls off quickly. If you need to reduce volume further, use a stronger insert — moulded pulp or a die-cut corrugated fitment — rather than simply tightening the box.
Consider a range of sizes. A single shipper for a whole catalogue is easy to buy and expensive to ship. Three sizes keyed to your order profile usually costs less in total freight than the extra SKUs cost in procurement. For e-commerce pack-out strategy see shipping packaging solutions.
Pallet Patterns and Stacking: Why Boxes Fail at the Bottom
When a pallet collapses, the bottom layer fails first. That is not a defect in the bottom boxes — it is the cumulative load of everything above them, plus whatever the pallet itself did wrong.
Stacking strength is time-dependent. A box’s compression rating is measured under controlled conditions over a short test. In a warehouse it carries load for weeks, and corrugated creeps: sustained load plus humidity progressively reduces the strength that was there on day one. A box rated for the static load can still fail after a month in a humid warehouse.
Alignment is worth more than board grade. Boxes stacked corner-to-corner transfer load through the strongest part of the structure. Boxes stacked with an overhang transfer it through the middle of the panel, where the board has almost no column strength. A well-aligned pallet of lighter boxes outperformed a misaligned pallet of heavier ones in almost every damage study you will find.
Pallet overhang is the most common error. A box hanging over the pallet edge by even 50 mm loses a large share of its effective strength, because the unsupported section bends under load. Match the box footprint to the pallet footprint, or accept the loss and buy more board.
Interlocking patterns and stretch wrap. Column stacking is strongest for compression but least stable in transit; interlocked patterns trade some compression strength for much better stability. Stretch wrap is what makes an interlocked pattern safe — it provides the horizontal restraint the pattern lacks. Wrap tension matters: too loose and the pallet racks, too tight and it crushes the top layer of boxes.
Related Solutions
Explore more custom-printing guides from our team: